

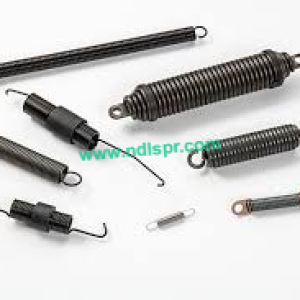
Assemblies requiring compact motion control frequently incorporate specially contoured metal filament to produce both pivoting action and retention without additional fasteners. Facilities such as ndlspr manufacture Wire-Form Spring elements whose free arms swing about a formed radius to create continuous torque while a hooked segment simultaneously engages a mating stop. The single continuous length of material stores energy solely through bending stress rather than helical coiling. How does this geometry manage to open freely under modest external pressure yet lock securely once the external pressure disappears?
Elastic recovery originates in the crystalline structure of the chosen alloy. When the arms rotate relative to the central bend, individual lattice planes shift within safe limits and generate an opposing moment that attempts to restore the original free shape. That opposing moment appears to the user as a gentle closing force on a lid or a firm seating force against a panel edge. Because the stress remains distributed along a continuous curve rather than concentrated at discrete coils, the element occupies less axial space than a conventional torsion unit of comparable output. Designers therefore favor the approach whenever packaging volume is restricted yet predictable return motion remains essential.
Latch behavior arises when one free extremity is shaped into a shallow hook or ramp. Application of an intentional force deflects the curved mid-section just far enough for the hook to clear an opposing shoulder. Upon release of that force the mid-section recovers and the hook seats behind the shoulder, preventing reverse travel. Disengagement follows the reverse path: a deliberate push or pull again deflects the mid-section until the hook clears the shoulder and the panel swings free. The absence of separate catch plates or riveted pins eliminates fretting surfaces that would otherwise generate particulate debris under vibration.
Alloy choice governs both the magnitude of available torque and the number of safe cycles. High-carbon grades deliver elevated tensile values that support larger deflection angles before permanent set appears. Stainless compositions resist oxidation when the surrounding atmosphere contains moisture or mild chemical vapor. Phosphate or nickel coatings may be applied after forming to further isolate the surface from corrosive agents while simultaneously reducing friction at the contact zone with the mating shoulder. Diameter selection balances stiffness against the available packaging envelope; thicker filament raises output force yet demands larger bend radii to keep peak stress below the endurance limit.
In enclosure covers the same element often serves dual duty. One pair of arms provides the continuous closing torque while a third arm, formed at a different plane, acts as the latching hook. The resulting three-dimensional contour occupies a single mounting plane and requires only two attachment points. Automotive glove-box lids, medical-instrument cases, and portable electronic housings adopt this arrangement because the continuous filament tolerates the mixed loading of gravity, occasional impact, and thermal expansion without progressive loss of seating force. Vibration environments particularly benefit from the lack of loose secondary hardware that could otherwise loosen over time.
Forming equipment draws the filament from continuous coil stock, then progressively bends, loops, and cuts it to the required three-dimensional path. Computer-controlled slides establish each successive angle with repeatable accuracy so that free-arm positions remain consistent from piece to piece. Subsequent stress-relief heating stabilizes residual stresses introduced during cold working and locks the final geometry. Dimensional checks verify arm angles, hook height, and load at a defined deflection before the finished elements proceed to packaging. Surface inspection confirms coating integrity and the absence of tool marks that could initiate fatigue cracks.
When specifying such an element the engineer first records the required closing torque, the maximum opening angle, the available mounting volume, and the expected number of open-close events. From those data the bend radius, arm length, and filament diameter are iterated until calculated peak stress remains safely below the material endurance threshold. Prototype samples then undergo bench cycling to confirm that the measured torque stays within acceptable scatter and that the latch engagement force remains comfortable for the intended operator. Once the prototype satisfies all criteria, production tooling is locked and process capability studies ensure ongoing consistency.
Attention during the forming sequence also addresses end condition. Cut ends are typically rounded or otherwise finished so they cannot abrade adjacent plastic or painted surfaces. Attachment loops, when required, receive controlled radii that distribute clamping stress and avoid localized yielding under assembly torque. These refinements collectively extend functional life by removing stress concentrations that would otherwise become initiation sites for fatigue.
Engineers seeking ready geometries for similar dual-function service can review the range of Wire-Form Spring options offered by ndlspr at https://www.ndlspr.com/ and then discuss envelope dimensions, alloy preference, and surface treatment with the technical staff. Direct collaboration allows adjustment of arm angles and hook profiles to match exact mounting features while preserving the calculated stress margins required for the intended service life.