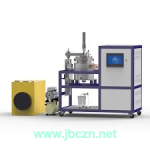
Selecting suitable stage dimensions constitutes a foundational step when organizing diamond synthesis runs that depend on microwave plasma activation. Inside MPCVD diamond deposition coating equipment connected with jbczn the available platform area governs how many seed crystals can be processed together and the maximum lateral span of continuous films. Operators therefore examine chamber geometry, plasma distribution patterns and thermal management capabilities before finalizing any configuration. What primary design elements usually establish the usable substrate capacity in standard systems?
Chamber architecture establishes the outer limit for stage placement. Resonant cavities built to sustain stable microwave modes accept circular or rectangular holders whose diameters stay compatible with the electric field profile. Expanded platforms require correspondingly larger plasma volumes so that radical density remains homogeneous from the center outward. Designers weigh cavity diameter against microwave frequency and power coupling to prevent secondary discharges or edge overheating that would otherwise reduce film quality near the boundary.
Plasma uniformity across the selected stage receives ongoing attention throughout process refinement. Microwave energy couples into the process gas mixture and creates a luminous region whose volume must fully enclose every seed or wafer section. Changes to pressure, gas composition and input power reshape this volume so growth rates stay consistent. When the platform enlarges, extra diagnostic ports or optical emission monitoring verify that radical concentrations do not decline at outer positions.
Thermal management systems interact closely with stage dimensions. Substrate holders incorporate water-cooled channels or radiant heaters that hold the narrow temperature window needed for ordered lattice formation. Larger platforms introduce greater thermal mass and possible gradients, prompting multi-zone heating or advanced pyrometry to keep surface conditions inside tolerance. Effective heat removal also shields seals and optical windows from prolonged high-temperature exposure.
Seed placement strategies further set practical capacity. Circular stages commonly arrange multiple single-crystal plates in concentric rings while rectangular platforms suit mosaic growth or continuous film deposition on wafers. Spacing between seeds accounts for plasma edge effects and gas-flow patterns so each crystal receives comparable radical flux. Holders that allow vertical adjustment fine-tune immersion depth inside the plasma region and thereby refine local growth conditions.
Gas delivery and exhaust arrangements scale with platform area. Mass-flow controllers supply hydrogen, methane and optional dopants through distributed injectors that keep partial pressures uniform. Exhaust ports positioned to encourage laminar flow avoid recirculation zones that might collect non-diamond carbon. When stage dimensions increase, fluid-dynamics modeling guides injector redesign so residence times and precursor concentrations remain balanced.
Automation and recipe handling adapt to differing capacities. Programmable controllers store sequences that adjust power ramps, pressure set-points and temperature profiles according to the loaded arrangement. Optical access windows and residual-gas analyzers deliver real-time feedback that operators use to confirm process stability regardless of seed count. Logging data across successive runs builds a library of proven parameters for each stage size.
Maintenance intervals also reflect platform scale. Larger chambers call for correspondingly thorough cleaning of internal surfaces and verification of microwave transmission components after extended campaigns. Seed-holder exchange procedures stay standardized, yet the physical size of components influences the time required for reassembly and leak checking. Facilities schedule these tasks to coincide with planned target changes and thereby limit interruption of production sequences.
Process results connect directly to the chosen capacity. Uniform single-crystal growth across multiple seeds supports higher aggregate yield when the plasma remains stable. Continuous polycrystalline films benefit from stages that match the intended wafer diameter so subsequent polishing and cutting steps encounter consistent thickness. Aligning stage size with downstream requirements therefore reduces material waste and simplifies quality inspection.
Facilities prepared to manage varied platform requirements within MPCVD diamond deposition coating equipment such as those linked to jbczn provide chamber designs that accommodate both multi-seed single-crystal runs and continuous film growth on expanded stages, and complete equipment details appear at https://www.jbczn.net for examination before formal technical inquiries.